Finite Capacity Scheduling: A Guide for the Shop Floor
2026-11-17
Finite capacity scheduling is planning production within the actual limits of machines, people, and shifts, so that an order is scheduled only when the resources to manufacture it are available. If they are not, the delivery date moves in the plan, not on the shop floor. It works only to the extent that the starting data is reliable: a perfect schedule based on made-up times is still a false schedule. That is why, in a manufacturing SME, the key is not just the algorithm, but getting production, purchasing, warehousing, and maintenance to work from the same picture of the plant. At Bold Factory, we bring these four areas (MES, MRP, WMS, and GMAO) together on one platform, and in this guide we explain how to apply finite capacity without setting up a never-ending project.
In brief
-
Finite capacity respects each resource's limits and pushes back the delivery date when there is no room; infinite capacity loads orders without checking whether they fit.
-
Sequencing determines the order of jobs within that limit: it is the part of the problem that is most noticeable in the day-to-day running of the shop floor.
-
The plan is credible only with real data: times, stoppages, maintenance, materials, and shifts, captured on the shop floor rather than estimated in an office.
-
Rescheduling after every deviation creates distrust: it is better to set rules, triggers, and a frozen window.
-
The more departments share data in a single system, the less the plan is disrupted by information that arrives late.
Table of contents
What finite capacity scheduling is
Every production resource has a ceiling: a press runs a certain number of hours per shift, a qualified operator cannot be in two cells at once, and a machining machine stops for a tooling change. Finite capacity scheduling takes these limitations into account to calculate how much work can be produced in a given period. Microsoft Dynamics 365 defines it this way in its documentation: if there is not enough capacity, the delivery date is delayed and the job is scheduled when capacity is available.
That logic has an inconvenient and very useful consequence: the plan tells you the truth before the customer does. A delivery promise calculated with finite capacity is one the plant can meet, and that is what allows the operations manager to stop putting out fires and the sales team to stop promising lead times at random.
The names it goes by
In practice, you will hear several terms for the same thing: finite planning, finite capacity planning, or, in English, finite capacity scheduling. In an advanced planning system, people also talk about detailed scheduling, which takes the plan down to the machine level and sequences it.
Finite capacity versus infinite capacity
Classic MRP planning calculates what needs to be manufactured and purchased, and when, based on demand and bills of materials. By default, it assumes that resources can handle whatever is asked of them. That is infinite capacity: useful as a first approximation, but dangerous as a final commitment.
| Criterion | Infinite capacity | Finite capacity |
|---|---|---|
| Assumption about resources | There is always room | Each resource has a limit per period |
| What happens if there is overload | The load builds up and is discovered on the shop floor | The order is delayed or moved in the plan |
| Delivery date | Theoretical, based on fixed lead times | Calculated with the existing load already reserved |
| Typical use | First calculation of requirements | Schedule released to the shop floor |
| Data effort | Low | High: times, calendars, stoppages |
These are not opposing approaches. An academic study published in the International Journal of Production Research proposes a finite capacity heuristic that uses the sequence in which jobs are placed on machines as a link between the infinite-capacity and finite-capacity plans. Put simply: the infinite plan sets out the ideal, and the finite plan adjusts it to what is possible.
When it is not a good idea to use it
Microsoft's own documentation warns that if capacity changes with requirements, for example with variable shifts, the calculated times will not be correct. A plant with shifts that open and close depending on the order must first stabilize its resource calendar, or the schedule will be out of date from the start.
Job sequencing: the order within the limit
Finite capacity answers how much fits. Sequencing answers in what order. The two questions are connected: two orders that fit in the week can take different amounts of time depending on which is manufactured first, because tooling, color, or material changes depend on the sequence.
Operations research has distinguished these two areas for decades. An article from the Centre for Political and Constitutional Studies on linear programming and production scheduling separates resource allocation models, which decide what quantities to produce within fixed constraints, from sequencing models, which determine the order to minimize machine idle time.
Common priority rules
In a shop with several parallel machines, not every machine can make every item, and each one has its own setup times. A UPC thesis on this type of machine shop solves the sequence using a metaheuristic and rules such as EDD (earliest due date first) and SFT (shortest job first), with the goal of minimizing average tardiness.
In practice, three ideas are enough for an SME:
-
Earliest due date first (EDD): protects customer service.
-
Shortest job first: frees up the machine quickly and reduces work in progress.
-
Group by setup: run orders that share tooling or material back to back to save on changeovers.
No rule always wins. Choosing one means deciding what matters most to you, and it is best to decide in advance, not when two urgent orders are competing for the same machine.
The data the schedule needs
A finite schedule is only as good as the information that feeds it. The UPC study on job shop scheduling with limited buffers proposes describing the plant in terms of resources, layout, and production recipes, and includes requested and delivery dates, products and quantities in orders, and equipment characteristics as inputs. Translated to a shop floor, the minimum list is:
-
Resources and calendars: machines, cells, and qualified operators, with their actual shifts and holidays.
-
Routes and times: operations for each item, setup and cycle times for each machine, and which machines can manufacture which items.
-
Orders: quantities, delivery dates, and commercial priority.
-
Materials: actual inventory and purchase arrival dates, because an order without material is not a schedulable order.
-
Maintenance: planned stoppages and breakdowns that reduce available capacity.
-
Quality and rework: inspections and rejects that consume resource time.
The 100% utilization mistake
The most common mistake is counting theoretical hours. A CNC machine with 40 hours on the calendar does not have 40 hours of cutting time: setup, maintenance, tools, qualifications, and inspection all have to be deducted. Times need to be measured on the shop floor, by machine and by shift, and reviewed. A Vrolen article on scheduling optimization points out that the real constraint changes with the product mix, breakdowns, and staffing, so today's bottleneck may not be next week's.
How to build the schedule, step by step
The process is the same in a spreadsheet, an ERP, or a production platform. What changes is how much manual work each step requires.
-
Define the scope. Start with the area that hurts most: the bottleneck cell or the product family with the most delays. It is easier to expand later than to redesign everything.
-
Load the resources and their calendars. Available hours here should be reduced by planned stoppages. With the maintenance module (GMAO) on the same platform as production, maintenance stoppages are in the same system as the orders they affect.
-
Calculate requirements. MRP determines what to manufacture and purchase. Our platform integrates planning and purchasing (MRP) with production, so orders and purchases are based on the same information.
-
Schedule from the requirement date. According to Microsoft's documentation, planned orders are scheduled from the requirement date, taking already-reserved capacity into account; if they do not fit in the optimal calendar, the system tries to order the components earlier. You can see how we organize this level in our documentation on production plans.
-
Sequence the orders. Apply the rule you have chosen (due date, duration, grouping by setup) and check that the resulting order respects material availability.
-
Release the schedule to the shop floor and collect data. Operators record start, finish, stoppages, and rejects on tablets on the shop floor, using an interface designed for any operator to use. These records are what correct the times in the next cycle.
-
Measure and adjust. Compare what was planned with what was completed and correct times, calendars, and rules.
Step 6 is where most implementations break down: if shop-floor data is entered manually and only arrives the next day, the plan is always one day behind.
Rescheduling without creating anxiety
A breakdown, an urgent order, or a supplier failure means the schedule has to move. The opposite risk also exists: rescheduling after every deviation. Vrolen warns in its guide that doing so creates anxiety and a loss of confidence in the plan, and proposes setting rules with defined triggers, a frozen window, approval, and communication.
You can put this into practice in your plant with four decisions:
-
Frozen window: the nearest part of the schedule is not changed except for a serious reason. This lets the shop floor work calmly.
-
Triggers: a breakdown lasting longer than a certain time, a material that does not arrive, or an urgent order approved by management.
-
Owner: one person with the authority to approve changes, not a WhatsApp group.
-
Record every manual change: if the supervisor changes the order, the reason should be noted. These changes reveal constraints the model did not know about, such as shared tooling or a particular operator's skill.
Decide what you are optimizing before scheduling
Maximizing machine utilization can inflate work in progress; minimizing changeovers can delay precisely the urgent work. Agreeing in writing on what takes priority (service, flow, cost, or stability) saves arguments when the schedule has to make a choice.
Metrics to see whether it is working
You do not need a huge dashboard. Five metrics tell the story:
-
Schedule adherence: how much of what was scheduled is manufactured in the planned order and timeframe.
-
On-time, in-full delivery (OTIF): the plan's reflection in the customer experience.
-
Bottleneck load: if it is very low, capacity is being wasted; if it is very high, any incident disrupts the plan.
-
Rescheduling frequency: many changes in quick succession point to poor rules or data.
-
Work in progress and manufacturing lead time: if they fall, sequencing is helping flow.
Set your own baseline over a few weeks and compare against it afterward. Generic thresholds from other industries are of little use: what matters is your improvement against your starting point. Our control panel brings together this visibility for the operations manager and the owner who is not always on the shop floor.
When the spreadsheet falls short
Many factories schedule in Excel, and it works while operations are simple: one clear bottleneck, few open orders, and a plan that changes little. The breaking point depends less on company size than on complexity: several shared resources, alternative routes, changes that depend on sequence, and urgent jobs that require recalculating several times a day.
Signs that it is time to leave the spreadsheet behind:
-
The planner is the only person who understands the file, and when they are absent, the plan stops.
-
Times and stoppages are written down on paper and entered manually afterward.
-
Purchasing, warehousing, and maintenance work with data that does not match production's data.
-
Every urgent order means manually reworking half the schedule.
-
Lead times promised to customers do not come from the plan, but from intuition.
If two or three of these sound familiar, the problem is no longer the formulas. It is that the information is scattered across too many places.
Why it matters to have everything in one system
Systems designed for large companies handle scheduling with separate modules, consultants, and long projects. For an SME with between 5 and 100 operators, that complexity often outweighs the benefit. Bold Factory is a cloud platform that integrates production (MES), planning and purchasing (MRP), warehousing and traceability (WMS/SGA), and maintenance (GMAO/CMMS), with an interface operators can use on tablets. It can be implemented in a few weeks with no long-term commitment, and integrates by API with the ERP you already have; you can see the integration options.
The reason this matters for finite capacity scheduling is practical. The plan needs to know what material is available, which machine is stopped, and what has actually been produced. When that data lives in one system, the schedule is based on the reality of the plant, not a file someone updated on Monday. In addition, our AI agents automate repetitive tasks based on natural-language instructions, reducing the administrative burden on the planning team.
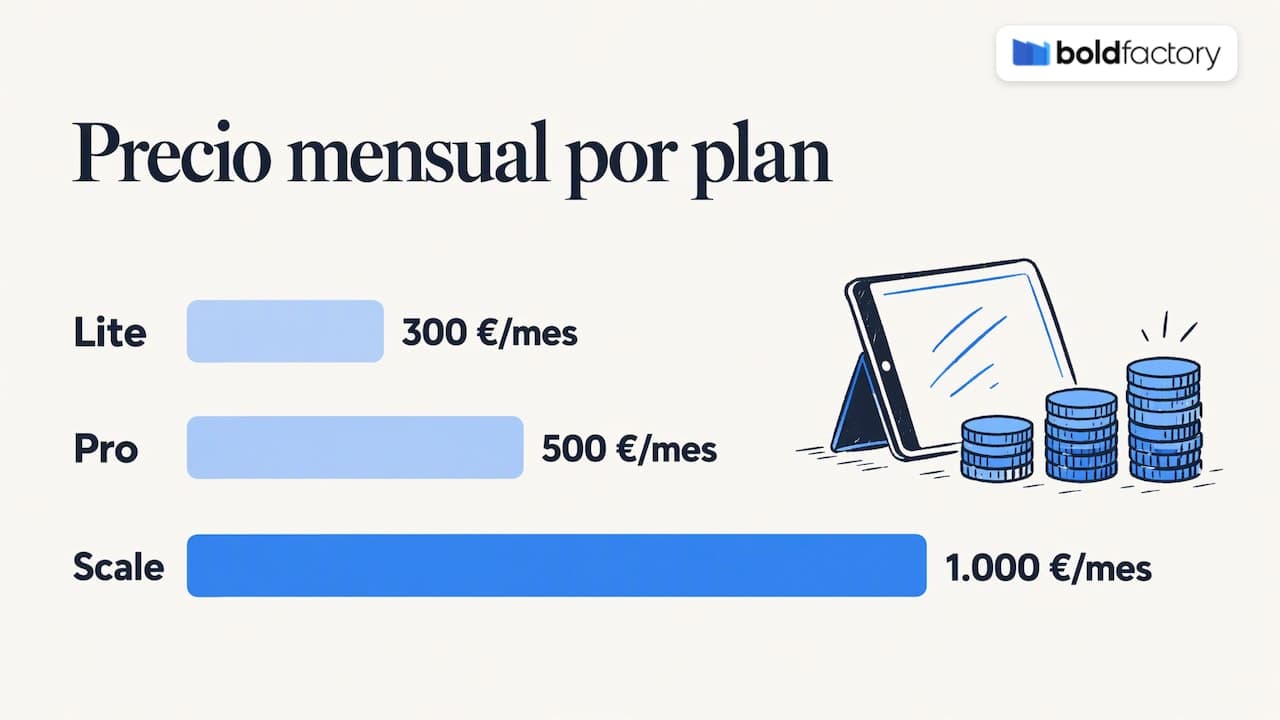
Plans have a published monthly subscription price, depending on users and features: Lite, at €300 per month; Pro, at €500 per month; and Scale, at €1,000 per month. You can start with what you need today and grow according to the team's actual needs.
How to get started without a long project
If you are going to take the step, our recommendation is not to try scheduling the whole factory at once.
-
Choose a decision that repeatedly causes friction. For example, which order goes first when two urgent orders are competing for the same machine. Resolve that one and then expand.
-
Digitize shop-floor data collection. Before optimizing anything, make sure actual times, stoppages, and materials are entered on a tablet.
-
Agree on the main objective and the rules for changes. Share them with the shop floor and sales.
-
Review after a few weeks. Compare theoretical times with measured times and adjust calendars.
The getting started guide in our documentation is a starting point for configuring the platform.
Frequently asked questions
Does finite capacity scheduling replace MRP?
No, it complements it. MRP calculates what to manufacture and purchase, and when; finite capacity scheduling checks that those orders fit into the actual resources and sequences them. They work best when they share the same order, material, and production data.
What is the difference between scheduling and sequencing?
Scheduling means assigning each order to a resource and a period while respecting capacity. Sequencing means deciding the order of the jobs on each resource. In practice, they are solved together because the order changes setup times and, with them, the capacity that remains.
How much data do you need to get started?
The data for the area you want to improve is enough: machines and calendars, routes with times, orders, materials, and stoppages. It is better to start with data measured on the shop floor for one bottleneck than with estimates for an entire factory.
Does it work in a plant with lots of urgent orders?
Yes, as long as you define rules for them. A frozen window, clear triggers, and one person to approve changes let you absorb urgent orders without rebuilding the schedule every hour.